
 EN

How Do Industrial Laser Cutting Machines Save Energy in Production?
They can, and the savings come from more places than the laser source itself. Fiber laser technology converted electrical power into beam energy several times more efficiently than the CO2 machines it replaced, and that single change rewrote the energy profile of laser cutting. Around the source, servo drives, nesting software, idle-power management, gas selection, and fume extraction all contribute to the total draw. An industrial laser cutting machine operated with attention to these variables consumes materially less energy per part than one run with default settings and loose scheduling, and the difference appears on the electricity bill long before it appears anywhere else.
Real-World Industry Case / Scenario
A Job Shop Measuring Energy per Part
A contract fabricator running two shifts decided to measure energy consumption per part rather than per month. The shop installed sub-meters on its industrial laser cutting machines and tracked kilowatt-hours against produced parts for three months. The first finding was unsurprising: the industrial laser cutting machines idled between jobs at high draw because operators left sources and extraction running through setup. The second finding was more interesting: nests produced by experienced programmers used 8% to 12% less material and correspondingly less cutting energy per finished part than nests produced with default spacing, because common-line cutting and tighter part arrangement reduced total travel and cut length.
The shop introduced three practices. Idle-power management put sources, extraction, and chillers into standby between jobs rather than leaving them at operating state through setup and material handling. Nesting review became a scheduled step, with programmers required to document material utilization per sheet. Assist gas selection was reviewed job by job, since the shop had been defaulting to nitrogen for carbon steel parts that oxygen cutting would have processed faster and cheaper. Within two quarters, energy per part on the industrial laser cutting machines had fallen by roughly a fifth, and the changes had required no capital expenditure.

Risk & Failure Mode Analysis
The Hidden Cost of Idle Operation
Laser machines draw significant power even when not cutting. Sources maintain readiness, chillers circulate, and fume extraction runs continuously unless managed. In shops where setup, material handling, and programming occupy a large share of machine time, idle draw can rival cutting draw. The risk is not dramatic failure but silent waste, which is why idle-power management, automatic standby, and scheduling discipline matter for an industrial laser cutting machine. Measuring consumption by machine state, rather than in aggregate, exposes where the energy actually goes.
Energy efficiency degrades quietly as components wear. Contaminated optics reduce power delivered to the workpiece, which forces the industrial laser cutting machine to work harder or run slower to complete the same cut. Loaded fume extraction filters increase fan draw, and a struggling chiller raises source temperature until output drops or the machine trips. Each condition converts clean energy into heat and lost production rather than into cut parts. The corrective discipline is maintenance: optics inspection on schedule, filter replacement on pressure drop, and chiller service, all of which keep the industrial laser cutting machine operating at the efficiency its design intended.
Technical Principles & Standard Compliance
Fiber Source Efficiency and System Draw
Fiber laser sources convert electrical input to optical output at wall-plug efficiencies in the range of roughly 25% to 35%, several times the efficiency of the CO2 technology they replaced. That efficiency advantage is the foundation of energy savings in modern laser cutting, but total machine draw includes much more than the source: motion drives, cooling, extraction, control systems, and assist gas generation all consume energy. Engineering teams evaluating an industrial laser cutting machine on energy performance should therefore compare total consumption per part or per kilogram of processed material, not source efficiency alone.
Nesting, Gas Strategy, and Measurement
Nesting software influences industrial laser cutting machine energy through material utilization. Higher utilization means fewer sheets per part, which means less cutting, less travel, and less idle time per finished part. Assist gas strategy is the second lever: oxygen cutting on carbon steel adds exothermic energy and reduces electrical demand, while nitrogen cutting costs more in gas compression and consumption. Measurement makes both levers visible: sub-metering by machine, logging consumption against production, and reporting energy per part gives operations teams the feedback that sustains the savings. Shops that publish these figures internally treat energy with the same discipline as material scrap.
Actionable Buyer & Maintenance Guide
Specifying an Industrial Laser Cutting Machine for Energy
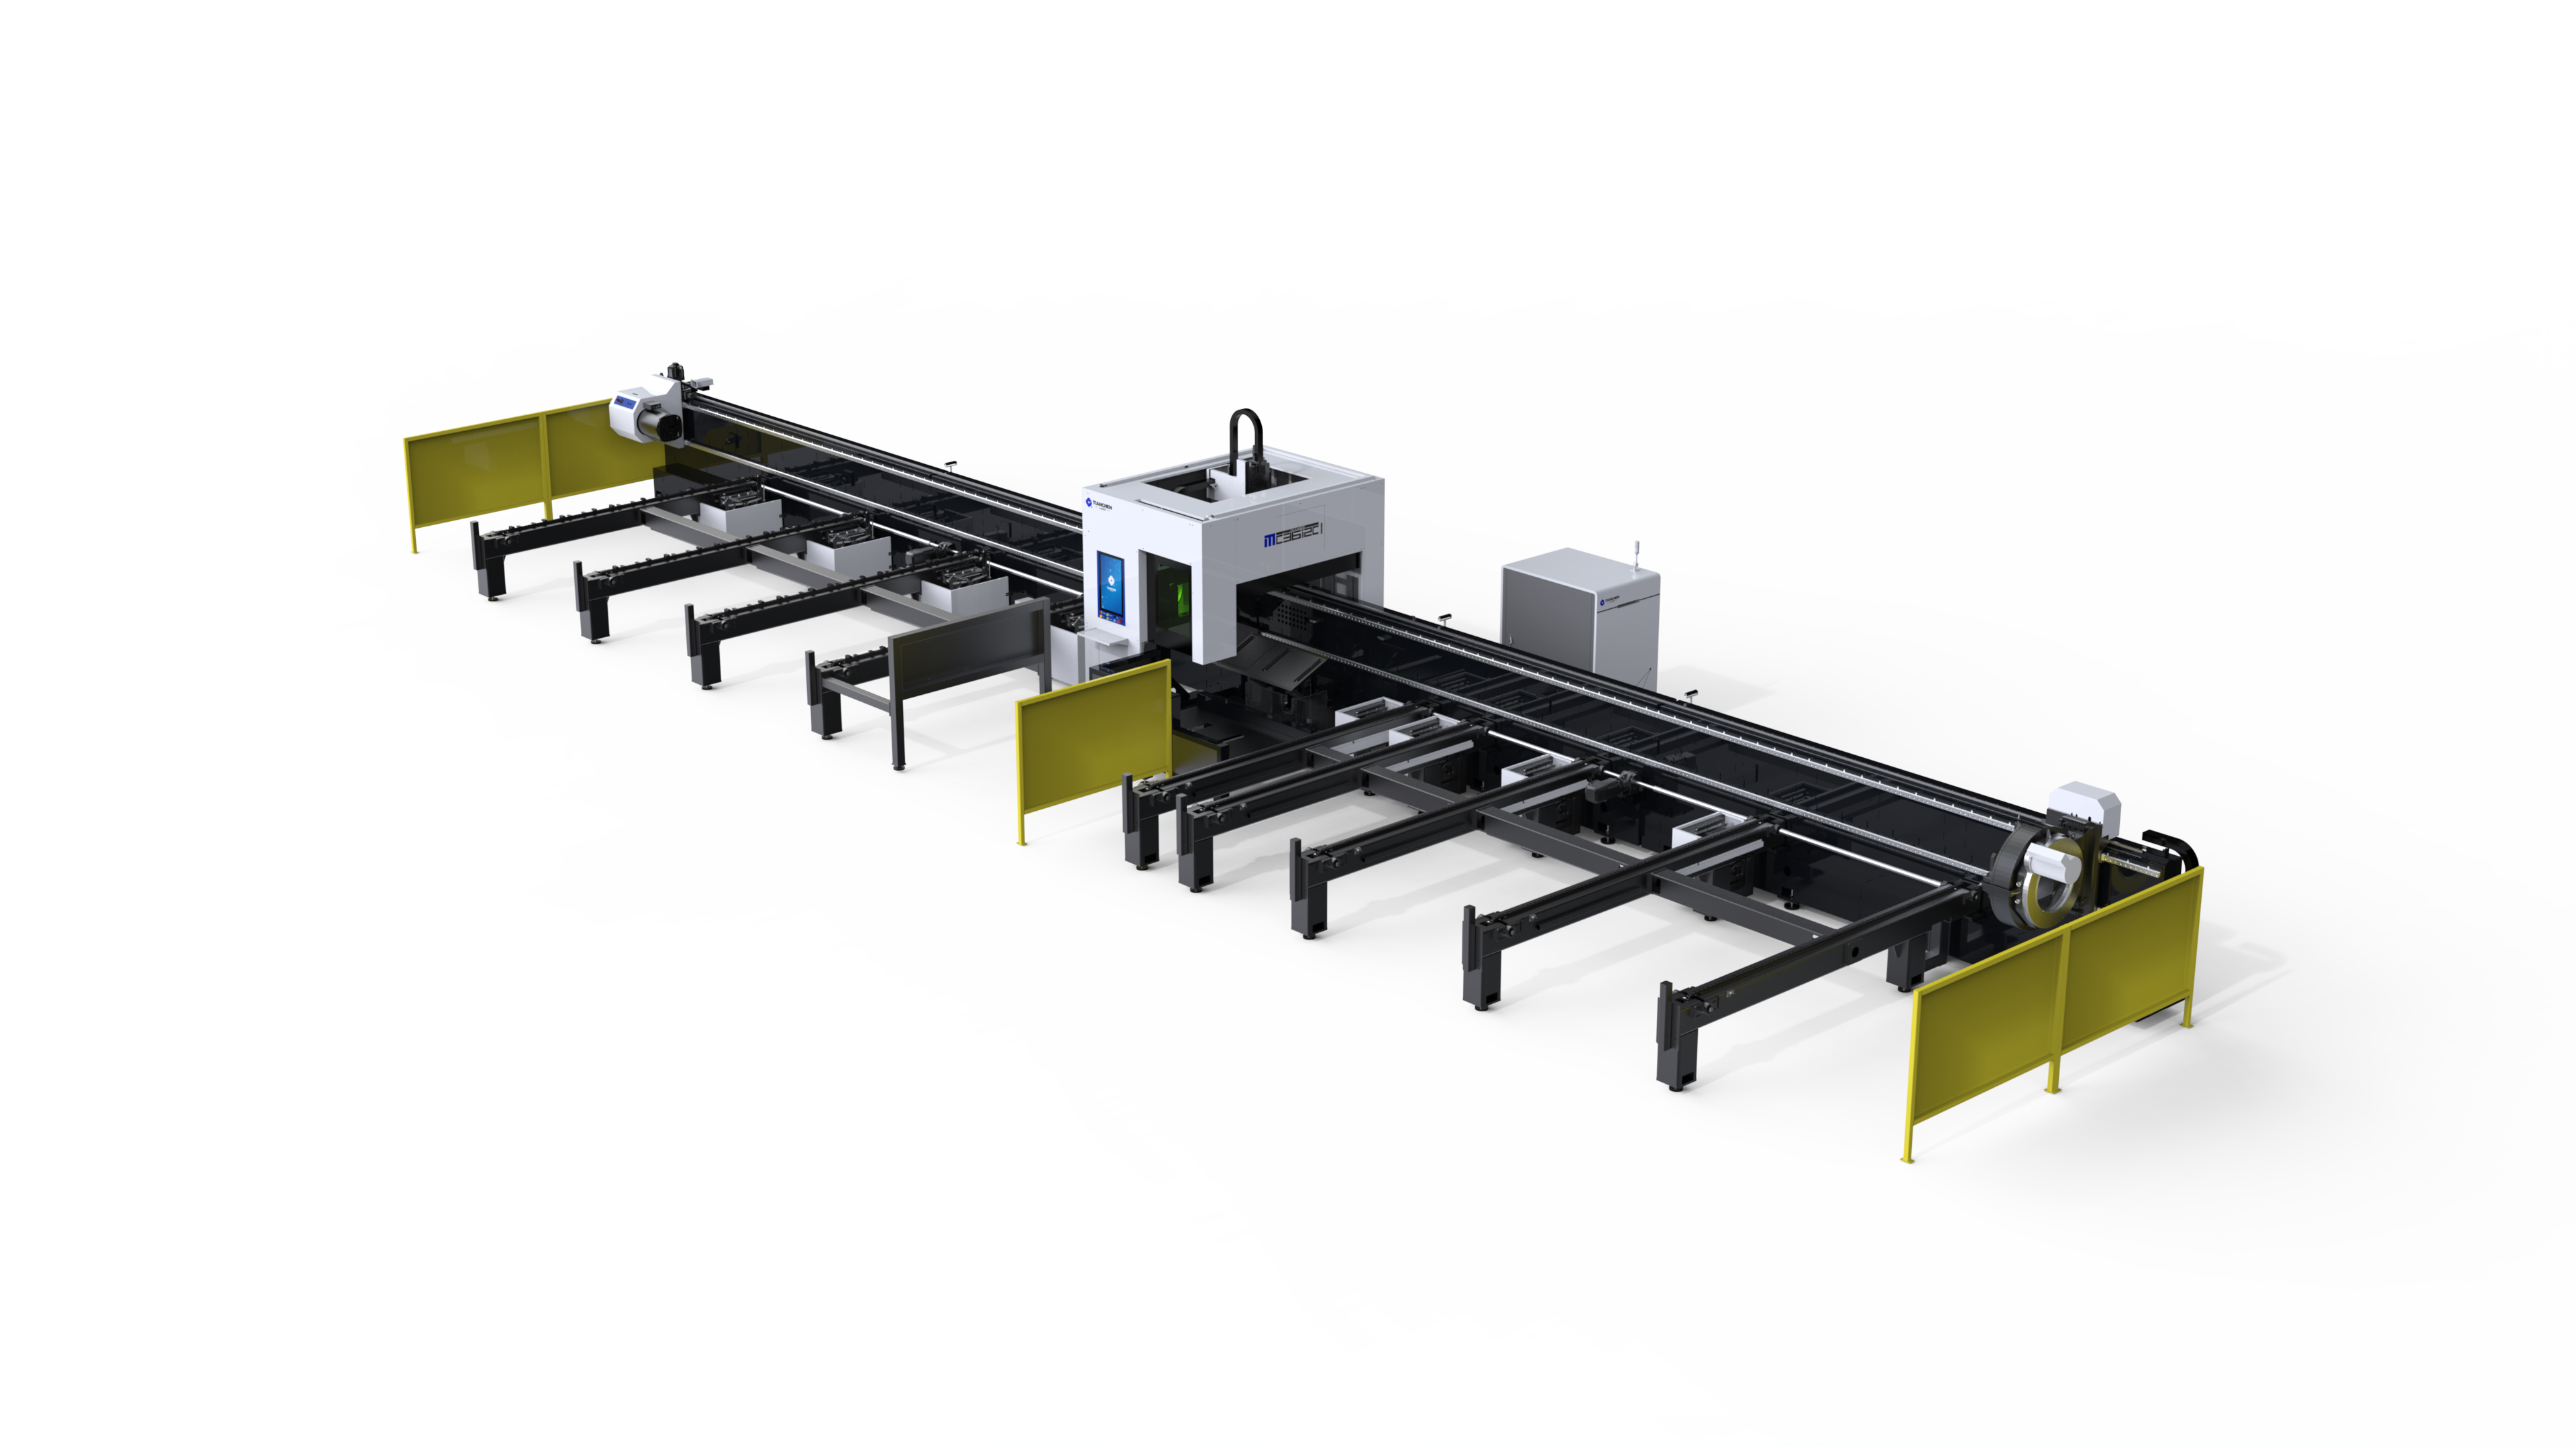
Buyers comparing machines should request documented energy consumption data under representative cutting conditions, not idle ratings. Useful comparisons include kilowatt-hours per hour of cutting, per sheet, and per kilogram of processed material, along with standby draw and recovery behavior. Features that support low energy operation include automatic standby, servo drives with energy recovery, efficient chiller design, extraction with demand-based control, and nesting software that reports material utilization. Machine suppliers such as Jinan-based Tianchen Laser provide performance data and application support that allow an industrial laser cutting machine to be compared on evidence rather than on marketing claims.
Operating Practices That Reduce Consumption
Operational discipline delivers savings without capital expense. Scheduling jobs to minimize setup and idle time, enforcing idle-power standby between jobs, reviewing nests for material utilization, and selecting assist gas by part requirement rather than habit all reduce consumption per part. Maintenance protects the gains: clean optics deliver source power to the workpiece instead of losing it as heat, and serviced extraction and cooling systems avoid the parasitic draw of degraded components. Tracking energy per part alongside cost per part turns these practices into a managed metric that survives staff changes.
Frequently Asked Questions
Question 1: How much energy does a laser cutting machine use per hour?
Answer: Consumption varies widely with source power, material, assist gas, and operating state. Higher-power fiber machines draw more while cutting but process material faster, so consumption per part or per kilogram is the meaningful comparison for an industrial laser cutting machine. Idle draw is also significant, since sources, chillers, and extraction maintain readiness, which is why standby management between jobs materially affects total energy use in a two-shift operation.
Question 2: Are fiber laser cutters more efficient than CO2 machines?
Answer: Yes. Fiber sources convert electrical input to beam energy at wall-plug efficiencies around 25% to 35%, several times higher than CO2 technology, and they avoid the gas consumption and maintenance that CO2 systems required. Total machine efficiency still depends on motion drives, cooling, extraction, and assist gas, so an industrial laser cutting machine should be compared on total energy per part rather than on source efficiency alone.
Question 3: How does nesting software affect energy consumption?
Answer: Nesting affects industrial laser cutting machine energy through material utilization and cut length. Tighter nests with common-line cutting reduce total cutting travel and increase parts per sheet, which lowers energy per finished part as well as material cost. Shops that review nests and document utilization typically find measurable gains without any equipment change, and the same discipline reduces idle time per part across the production schedule.
Question 4: What maintenance keeps a laser cutter energy efficient?
Answer: Optics inspection and cleaning on schedule, since contaminated optics waste source power as heat and force slower cutting. Fume extraction filters should be replaced on pressure drop, because loaded filters increase fan draw. Chiller service protects source temperature and output. Together these practices keep an industrial laser cutting machine delivering its rated power to the workpiece, which is where efficiency is either preserved or quietly lost.